Intelligent molecular-filtration cabinets for chemical handling and storage
Filtered Ductless Safety Cabinets
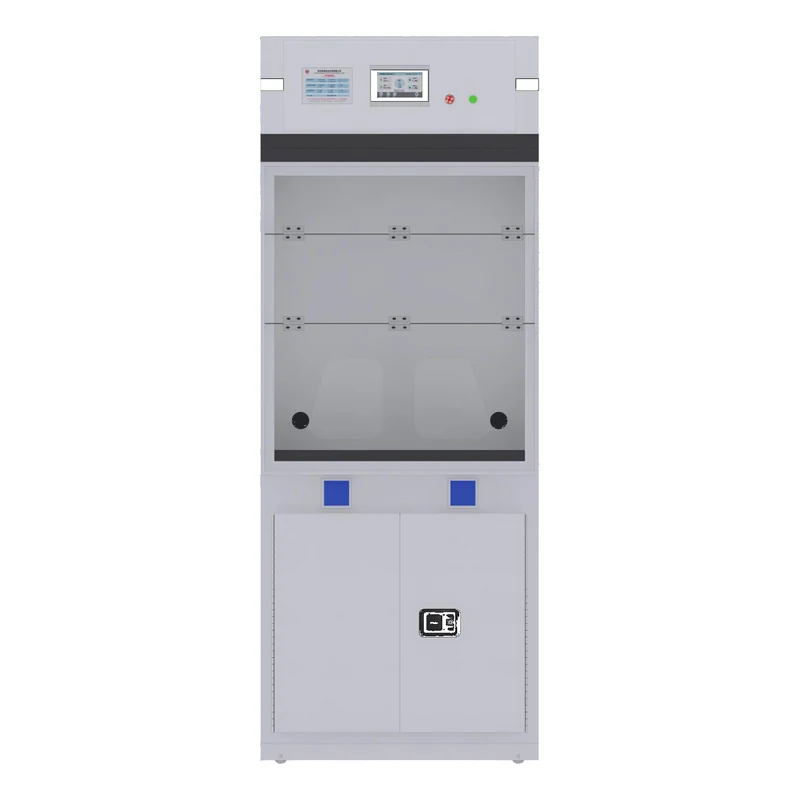
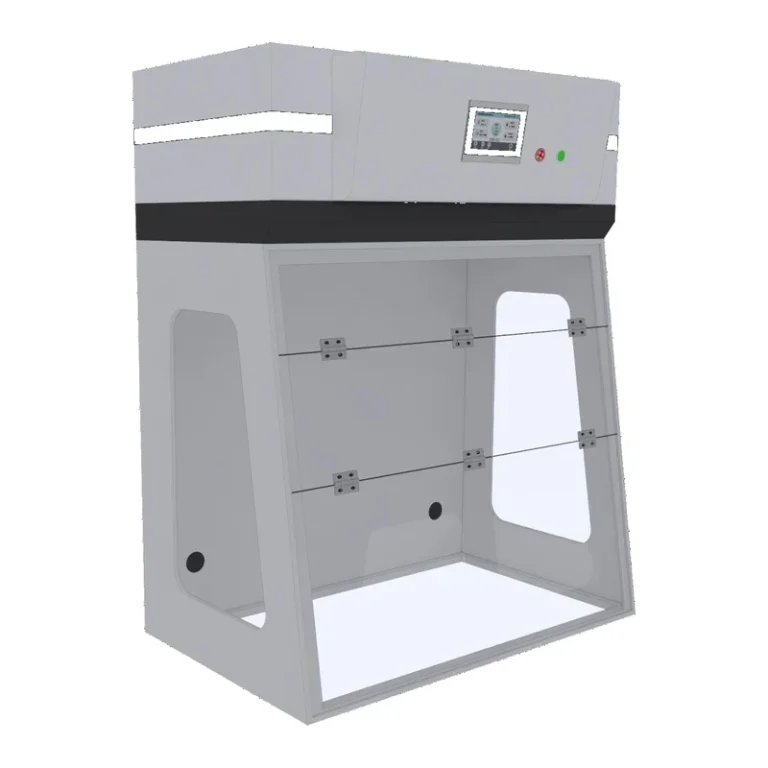
The intelligent ductless filtered safety cabinet is the filtration end of the fume hood spectrum taken to its conclusion: a sealed, negative-pressure enclosure whose dual carbon beds scrub the chemical load from the air and return it clean, with dual VOC probes watching the exhaust and the room, and a saturation alarm that announces the end of filter life before the chemistry does. The platform is built around molecular filtration. The dual-layer activated carbon — with impregnated media for acid gases, ammonia and formaldehyde classes — adsorbs more than 500 common laboratory chemicals, documented against a published compatibility chart. Filter bays are modular: a liquid-phase configuration for solvents, a dust configuration for powders, a mixed configuration for real work. The 7-inch touchscreen runs temperature, humidity, fan state and both VOC channels with integrated alarming and logged history. It doubles as chemical storage: the negative-pressure chamber holds bottles and reagents under continuous filtration, so the cabinet that protects your weighing also stores the chemicals — safely, monitored, duct-free. Send us the chemical inventory and the workflow, and we will configure the filter set and the alarm thresholds.
- 1Products
- 0Direct categories
- Technical support
-
Intelligent Ductless Filtered Safety Cabinet
- Model
- Intelligent ductless filtered safety cabinet (DNJQ series)
- Widths
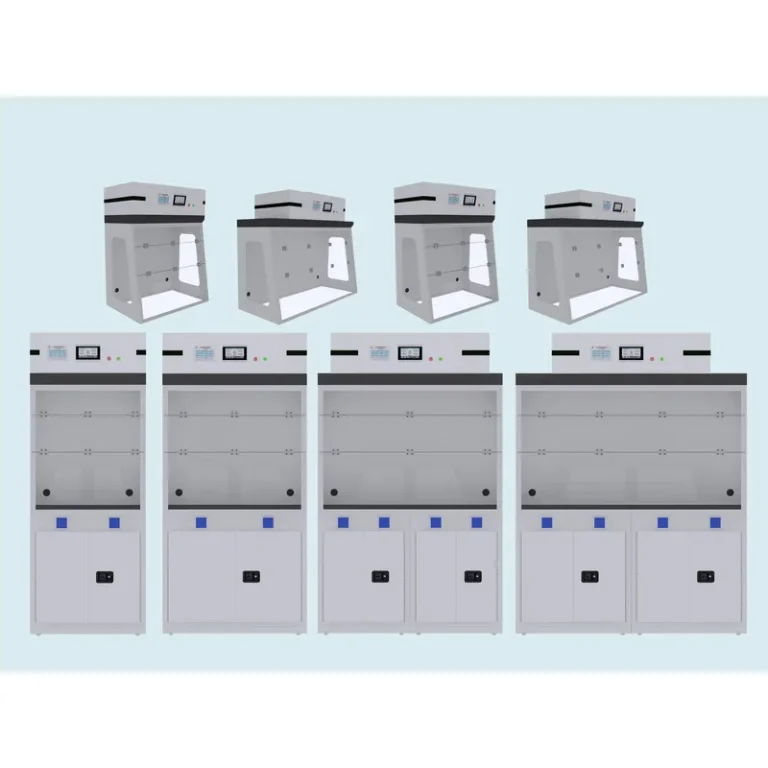
- 800 / 1000 / 1275 / 1600mm (benchtop and floor-standing models)
- Body
- ≥1.2mm steel, epoxy powder coated, chemical-resistant finish
- Front and side panels
- ≥6mm acrylic, transparent
Price on request
TECHNICAL DATA
Engineering the intelligent cabinet
The body is ≥1.2mm steel with epoxy powder coating and a chemical-resistant finish; front and side panels are ≥6mm acrylic for full visibility of the working plane and the stored inventory. A PSC fan runs continuous duty at 39-40 dBA. The platform is JG/T 385-2012 compliant, with face velocity 0.4-0.6 m/s at the working opening and 8-12 filter modules by model — 235 to 690 m³/h of purified air.
Filtered Ductless Safety Cabinets
View ProductIntelligent Ductless Filtered Safety Cabinet
- Model
- Intelligent ductless filtered safety cabinet (DNJQ series)
- Widths
- 800 / 1000 / 1275 / 1600mm (benchtop and floor-standing models)
- Body
- ≥1.2mm steel, epoxy powder coated, chemical-resistant finish
- Front and side panels
- ≥6mm acrylic, transparent
- Display
- 7-inch LCD touchscreen
- Monitoring
- Temperature, humidity, dual VOC concentration, fan state, filter status
- Alarms
- Filter saturation (user-set) · fan failure · setpoint deviation
- Filtration
- Dual-layer activated carbon + HEPA; modular liquid / dust / mixed configurations
- Air handling
- 235-690 m³/h by model; face velocity 0.4-0.6 m/s
- Fan
- PSC, 24-hour duty, 39-40 dBA, 82-218W
- Power
- 220-240V, 50-60Hz
- Compliance
- ASHRAE 110, UL 1805
- Width
- 1200mm
- Material
- Steel + Dual Carbon
- Form Factor
- Floor-Standing
Applications
Where filtered safety cabinets work
Monitored chemical handling and storage, duct-free.
Chemical storage under continuous negative-pressure filtration
Histology, pathology and staining workflows
Pharmacy compounding support and drug handling
Quality control dispensing and sample preparation
Any interior room where ductwork cannot reach
PERFORMANCE & SELECTION
What is a filtered safety cabinet?
A filtered ductless safety cabinet is a negative-pressure enclosure that combines the capture discipline of a fume hood with molecular filtration and chemical storage in one unit. Air enters through the working face or the storage chamber, passes the dual carbon beds and HEPA stage, and returns to the room purified. The negative pressure differential means nothing escapes unfiltered — vapour from opened bottles, dust from dispensing, whatever the inventory breathes.
- Negative pressure: nothing leaves unfiltered
- Dual carbon beds + HEPA stage
- Working enclosure and chemical storage in one
- Ductless — installs anywhere
CONFIGURATION & COMPATIBILITY
Dual carbon filtration and VOC monitoring
Two carbon layers double the adsorption path and split the workload: the first bed takes the bulk load, the second polishes the breakthrough. Dual VOC probes close the loop — one in the exhaust path watching breakthrough, one in the room watching the background — and the saturation alarm fires on your threshold, not after the fact. The controller logs exposure history so filter life is managed on data.
- Dual-layer carbon: bulk load + polish stage
- VOC probe 1: exhaust breakthrough monitoring
- VOC probe 2: room air quality monitoring
- User-set saturation alarm with logged history

IDENTIFICATION & TRACEABILITY
Clear Product Identification & Specification
Product names, model numbers, SKUs and option identifiers keep quotations, orders and internal records aligned.
- Product and model identification
- Option-specific SKU information
- Consistent quotation specifications
PRODUCT IDENTIFICATIONFiltered Ductless Safety Cabinets
- Catalog
- Laboratory equipment
- Products
- 1
- Selection
- Specification-led
Traceability
Traceability and documentation
Every filter, probe and alarm event is dated and archived.
- Filter batch, installation and change dates logged on the controller
- Chemical compatibility chart maintained against media
- Alarm and exposure history exportable for audit
- Serialised cabinet, fan and probe records
- Factory test data archived per serial number

Quality system
Quality system and factory testing
Alarm paths, probe response and filter integrity all tested at the factory.
ISO 9001 production line; JG/T 385-2012 compliant
Saturation alarm path function-tested
VOC probe response verified
Filter bed integrity check before dispatch
Serialised factory test report with each cabinet
Why WSHLab
Why laboratories choose the intelligent cabinet
Filtration, monitoring and storage engineered as one system.
500+ chemicals adsorbed on documented media
Dual VOC probes and saturation alarm — filter life on data
Negative pressure under fan-speed control
Working enclosure and monitored storage in one footprint
No ductwork; relocates with the workflow
OPTIONS & SPECIFICATIONS
Filtered Ductless Safety Cabinets Options & Specifications
Choose the format that suits your application, workload and handling requirements.
Dual-layer activated carbon filtration
Dual VOC probes with filter saturation alarm
Negative pressure control for chemical containment
Modular filters for liquid, dust and mixed loads
Adsorbs 500+ chemicals; 7-inch touchscreen monitoring
| Type | Capacity / Option | Material / Specification | Suitable Application | Storage / Handling |
|---|---|---|---|---|
| Dual-layer activated carbon filtration | By selected product | Product-specific configuration | Confirm with our team | Follow product guidance |
| Dual VOC probes with filter saturation alarm | By selected product | Product-specific configuration | Confirm with our team | Follow product guidance |
| Negative pressure control for chemical containment | By selected product | Product-specific configuration | Confirm with our team | Follow product guidance |
| Modular filters for liquid, dust and mixed loads | By selected product | Product-specific configuration | Confirm with our team | Follow product guidance |
| Adsorbs 500+ chemicals; 7-inch touchscreen monitoring | By selected product | Product-specific configuration | Confirm with our team | Follow product guidance |
Delivery and site
Delivery and installation
Pallet in, socket on, filters configured.
- 01
Ships assembled; two-person placement
- 02
220V/50Hz standard supply
- 03
Level floor; 30 cm service clearance
- 04
Filter media configured to your inventory before dispatch
- 05
Alarm threshold commissioning and training available; 12-month warranty

RECOMMENDATIONS
Related Products
Products frequently compared within this catalog.
Gallery
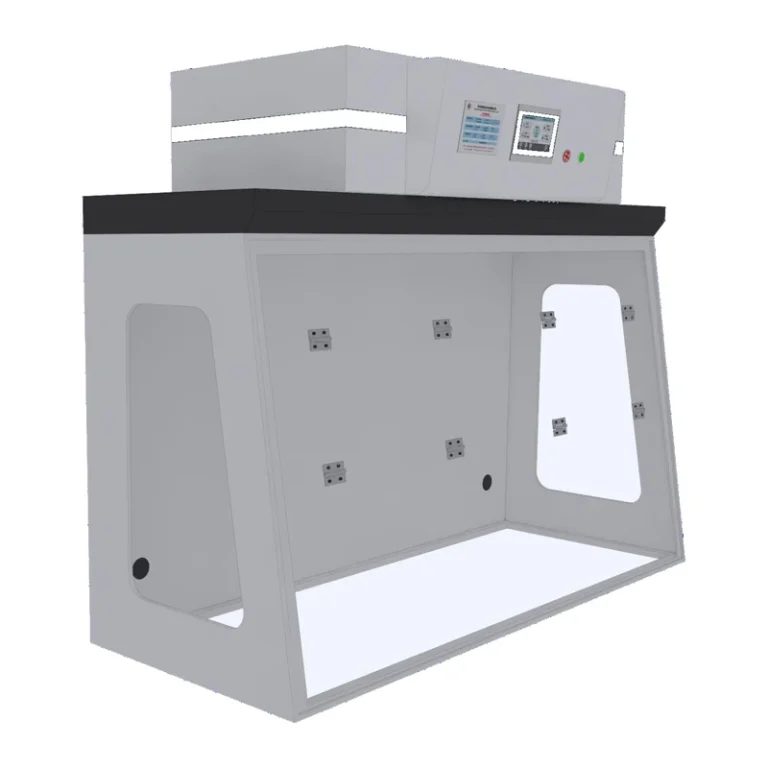
Intelligent filtered safety cabinets
The ductless filtered cabinet series from benchtop to floor-standing.
VIDEOS
Manufacturing & Quality Process
Category video library
Add category-specific video covers, titles, durations and video URLs in the Videos ACF section.
QUESTIONS & ANSWERS
Filtered Ductless Safety Cabinets: frequently asked questions
The questions buyers ask most often when specifying Filtered Ductless Safety Cabinets, answered by our technical team.
How many chemicals does it adsorb?
More than 500 common laboratory chemicals on dual-layer activated carbon, with impregnated media for acid gas, ammonia and formaldehyde classes — documented against a published compatibility chart.
Is there a filter alarm?
Yes — dual VOC probes monitor exhaust breakthrough and room air, feeding a user-set saturation alarm that fires before breakthrough, with the history logged on the controller.
Does it hold negative pressure?
Yes — the fan monitor adjusts speed to hold the negative-pressure differential as filters load; nothing leaves the chamber unfiltered.
Is it ductless?
Completely self-contained — no ductwork, no exhaust fan. Placement and a 220V socket are the entire installation.
Get a quotation
Request your filtered safety cabinet quotation
Send the chemical inventory and the workflow — weighing, storage or both — and we will configure the filter set, alarm thresholds and cabinet size, quoted within one working day.